What is a calibration adjustment policy?
People often treat “calibration” and “adjustment” as the same thing. They are not. A calibration compares your instrument with a reference standard of known, traceable value and records the difference, the as-found error. Adjustment comes after that: a technician turns a trim pot, writes new constants to firmware, re-zeroes a pressure gauge, or resets the click mechanism of a torque wrench so the reading moves closer to nominal. A calibration with no adjustment is still a complete calibration.
Because adjustment is optional, someone has to decide when it happens. If you don’t decide, the lab falls back on its own default procedure. That default may not match your quality system, your interval program, or your customer’s contract. An adjustment policy closes that gap. It is usually one short paragraph in your calibration procedure, repeated on each purchase order or quote request.
The question comes up most for adjustable mechanical and electrical instruments. In Techmaster’s ten-year record of 381,916 calibrations, torque wrenches (4,269), pressure gauges (2,378), and digital multimeters (more than 7,700) are among the highest-volume items. All three are routinely adjustable, so the policy question shows up on well over a thousand certificates a year.
Should the lab adjust an instrument that is already in tolerance?
The case for adjusting is simple. An instrument that reads +3.5% against a ±4% tolerance is technically in tolerance, but it has little margin left. Bring it back near zero and it has a full interval of headroom before it can drift out. For high-use torque tools on a production line, that headroom is often worth the extra labor.
The case against adjusting is less obvious but just as real. First, every adjustment resets the history. If the 10 V range of an 8.5-digit reference DMM reads +2 ppm today, it might read +4 ppm a year later and +6 ppm the year after. Left alone, that is a clean, predictable drift line you can use to set intervals and apply corrections. Re-zero it every year and the line disappears. Second, if the as-found deviation is about the same size as the lab’s expanded uncertainty, the lab can’t tell whether the deviation is real. Adjusting to that reading can move the instrument further from true value. Quality engineers will recognize this as over-adjustment, or “tampering”, which adds variation instead of removing it.
The practical answer is to decide ahead of time, by instrument class, which effect matters more to you: margin or history.
What are the three common adjustment policies?
Interval-analysis literature calls adjustment “renewal”, because adjusting an instrument renews its starting point. Each policy suits a different kind of equipment, and the table below compares them.
| Policy | When the lab adjusts | Main advantage | Main drawback | Typical fit |
|---|---|---|---|---|
| Renew-always | At every calibration, even when in tolerance | Maximum margin each interval; each interval starts near nominal | Erases long-term drift trend; more labor; risk of adjusting within the uncertainty | High-use production tools: torque wrenches, crimp tools, handheld DMMs |
| Renew-if-failed | Only when as-found is outside tolerance | Keeps a clean drift history; least handling of stable instruments | Instruments can sit near the tolerance limit for a whole interval | Reference standards, stable bench instruments, long-history assets |
| Renew-as-needed | When as-found passes a set adjustment limit, for example 70% of tolerance | Balances margin and history; adjusts only when it buys real headroom | Needs a defined limit per instrument class and a lab that applies it consistently | Most general test and measurement inventories |
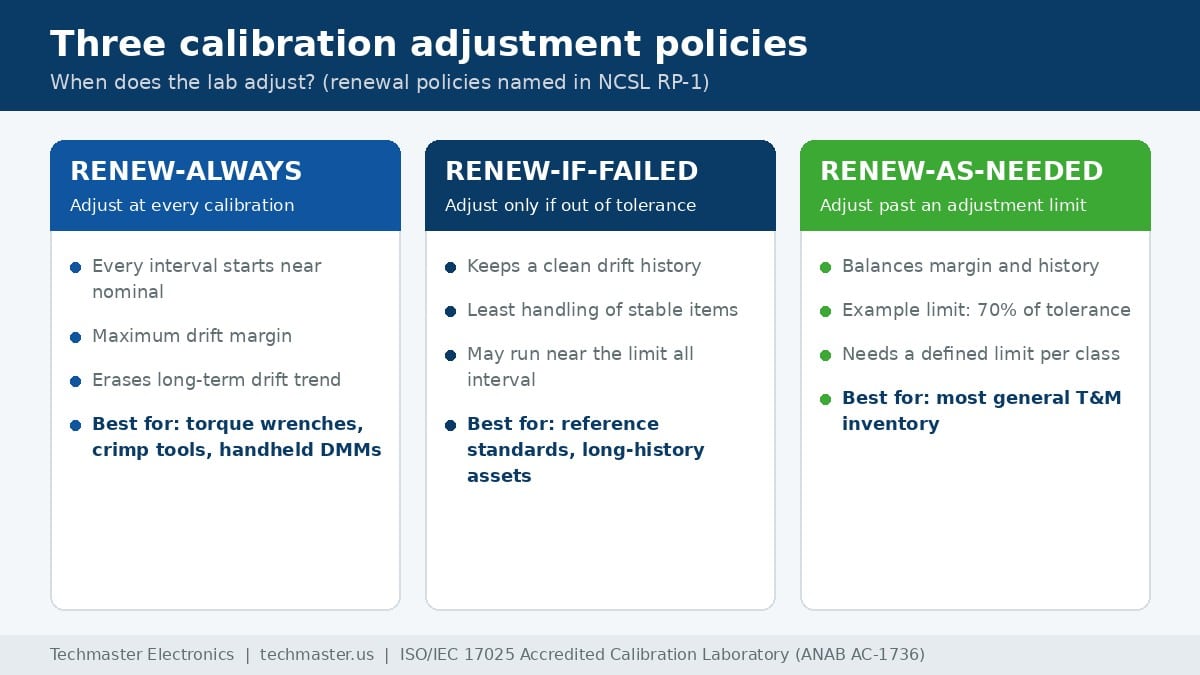
Many organizations combine them. They apply renew-if-failed to reference standards, renew-as-needed to general inventory, and renew-always to production tools whose tolerances are tight compared with how fast they drift.
How do you set an adjustment limit?
Start with two numbers you already have: the instrument tolerance and the lab’s expanded uncertainty (k = 2) for that measurement, which appears on an ISO/IEC 17025 certificate. Then look at past as-found results to see how far the instrument usually drifts in one interval. The adjustment limit sits between them. It should be above the uncertainty, so you never adjust on noise, and far enough below the tolerance that one interval’s typical drift can’t push the instrument out.
Here is a worked example for a torque wrench with a ±4% of reading tolerance and an adjustment limit set at 70% of tolerance (±2.8%):
| As-found error | Within tolerance (±4%)? | Past adjustment limit (±2.8%)? | Action under renew-as-needed |
|---|---|---|---|
| +1.1% | Yes | No | Report as-found; no adjustment; as-found = as-left |
| +3.1% | Yes | Yes | Adjust toward nominal; report as-found and as-left |
| +4.6% | No (out of tolerance) | Yes | Adjust or repair; report both; you start an impact assessment on product measured since the last calibration |
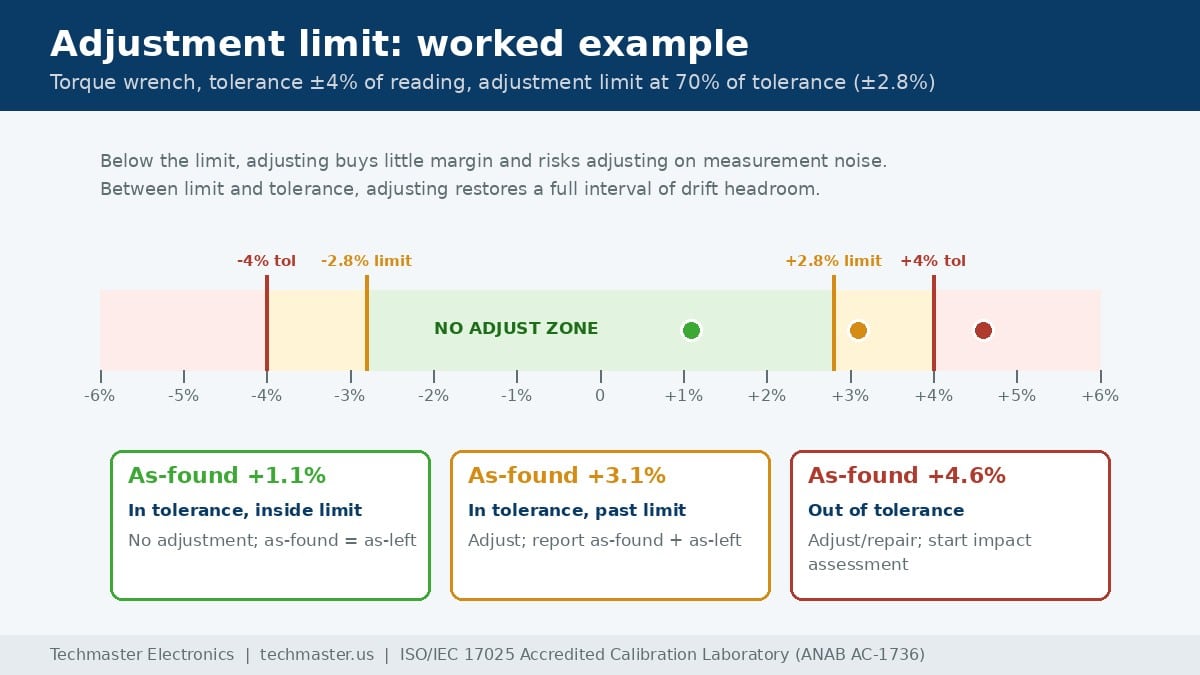
The 70% figure is an example, not a rule. A stable instrument with a generous tolerance can use a higher limit. One that drifts quickly or carries a tight test uncertainty ratio needs a lower one. Guard-banded acceptance (covered in our guide to calibration decision rules and guard banding) answers a different question: whether a reading counts as a pass or fail. The adjustment limit only decides whether to adjust, so keep the two separate in your procedure.
How does adjusting change your calibration interval data?
Interval methods in ILAC G24 (ILAC Guidance Series) and NCSL RP-1 rely on the as-found result at each calibration: was the instrument in or out of tolerance when it came in? NIST’s guidance on recommended calibration intervals says recalibration reports should include “as submitted” and “post calibration” data to validate and refine the interval. That data is only comparable from one calibration to the next if the adjustment rule stays the same.
Consider two identical pressure gauges on a one-year interval. Gauge A is re-zeroed every year, so each as-found shows one year of drift. Gauge B is never adjusted while in tolerance, so its as-found shows the drift added up since its last adjustment. After three years, B will look three times worse than A even though both drift at the same rate. If your interval software treats both histories the same way, it will read B’s drift rate as three times A’s and shorten B’s interval on the wrong evidence.
The fix is administrative: record on each calibration whether an adjustment was made. ISO/IEC 17025 certificates already separate as-found and as-left data when an adjustment happens, as explained in our quality manager’s guide to as-found vs as-left calibration data. Make sure that flag goes into your asset system. Then the reliability method in our guide to setting calibration intervals with ILAC G24 will give you defensible intervals.
What does ISO/IEC 17025 require when an instrument is adjusted?
Three clauses of ISO/IEC 17025:2017 matter here:
- 7.1, review of requests, tenders and contracts: the lab and customer agree on requirements before work starts. Your adjustment policy belongs here, which is why it should be written on the PO rather than assumed.
- 7.8.4.1, calibration certificates: where an instrument has been adjusted or repaired, the results before and after must both be reported, if available. That is the as-found / as-left pair.
- 6.4.12, equipment: the lab must take practical measures to prevent unintended adjustments from invalidating results. Tamper seals and protected settings are the usual controls.
If you also ask for a pass/fail statement of conformity, the decision rule must be agreed with you at contract review (clause 7.1.3) and applied and reported on the certificate (clause 7.8.6). When an instrument is adjusted, ask for a conformity statement on the as-found condition as well as the as-left one, because the as-found result tells you whether past measurements were at risk. An out-of-tolerance as-found triggers your own impact review, as described in our article on what to do with out-of-tolerance calibration results.
Techmaster Electronics has calibrated test equipment since 1989 and holds ANAB accreditation to ISO/IEC 17025 under certificate AC-1736. The accredited scope covers four US laboratories: Vista and Santa Clara, California; Orlando, Florida; and San Antonio, Texas. Details are on our ISO/IEC 17025 accreditation page.
When should you tell the lab not to adjust?
- Reference standards with long histories. A resistance standard, voltage reference, or gauge block set often gets its value from its certificate history, not its nominal value. Adjusting it, where adjustment is possible at all, breaks the record that makes it useful.
- Instruments you correct in software. If your test station applies correction factors from the last certificate, an unannounced adjustment makes those corrections wrong overnight.
- Deviation within the uncertainty. Adjusting on a reading the lab can’t resolve adds variation. Ask for no adjustment unless the as-found error clearly exceeds the expanded uncertainty.
- Sealed, validated, or regulated equipment. Devices with tamper seals, validated configurations, or legal-metrology marks may need authorization before anyone changes a setting.
- Instruments that keep failing. Repeated adjustment can hide a failing component. If an instrument needs large corrections every interval, a repair evaluation is usually better than another adjustment.
How do you write a calibration adjustment policy on a purchase order?
A clear instruction answers four questions: when to adjust, what data to report, whether to contact you before repair, and whether out-of-tolerance results need immediate notice. For example:
- “Reference standards: do not adjust if in tolerance. Report as-found data with uncertainties.”
- “General inventory: adjust if as-found exceeds 70% of tolerance. Report as-found and as-left data.”
- “Production torque tools: adjust to nominal at every calibration. Report as-found and as-left data.”
- “All items: notify us within one business day of any out-of-tolerance as-found result, and get approval before repair.”
Also make sure the calibration level you order produces data. Techmaster offers three levels: Traceable (certificate), Z540 (certificate and data report), and ISO/IEC 17025 (certificate, data report, and measurement uncertainties). Only the data-bearing levels give you the as-found numbers an adjustment policy depends on. For torque tools, pressure gauges, and other mechanical instruments, our ISO/IEC 17025 mass and mechanical calibration services report both data sets when an adjustment is made. Electrical instruments go through our ISO/IEC 17025 electrical calibration services. The full list of disciplines is on the Techmaster calibration services hub.
Key takeaways
- Calibration measures error. Adjustment is a separate, optional step that your policy should control.
- The three standard policies are renew-always, renew-if-failed, and renew-as-needed. NCSL RP-1 uses these names.
- An adjustment limit should sit above the lab’s measurement uncertainty and far enough below the tolerance to leave one interval’s drift margin.
- Adjustment policy changes what as-found data means. Record whether each calibration included an adjustment before you run calibration interval extension analysis.
- ISO/IEC 17025:2017 requires before-and-after results when an instrument is adjusted (clause 7.8.4.1). Whether to adjust is agreed with the customer.
Frequently asked questions
Is adjustment part of calibration?
No. Calibration determines the instrument’s error against a traceable reference. Adjustment is a separate operation that reduces that error. An instrument can be fully calibrated with no adjustment, and when nothing is changed the single reported result serves as both the as-found and as-left value.
Will an accredited lab adjust my instrument automatically?
It depends on the lab’s default procedure and on what you agree when the order is reviewed. To avoid surprises, write your adjustment policy on the purchase order or quote request, for example adjust only if out of tolerance, or adjust when as-found error exceeds a stated percentage of tolerance.
What is a good adjustment limit for calibration?
There is no single number. Many programs start at a fixed percentage of tolerance, such as 70%, then refine it. The limit should sit above the lab’s expanded measurement uncertainty and leave enough margin below the tolerance to absorb one interval of typical drift.
Does adjusting an in-tolerance instrument affect my calibration interval?
Yes. Adjusting resets the starting point, so each as-found result shows only one interval of drift. Not adjusting lets drift accumulate across intervals. Both are valid, but your interval analysis must know which policy applied to each calibration, or it will draw the wrong conclusions.
Should reference standards be adjusted during calibration?
Usually not while they are in tolerance. A reference standard’s value often comes from its certificate history and known drift rate, and adjusting it breaks that record. Most labs assign the calibrated value to the standard and apply corrections rather than physically adjusting it.
What does ISO/IEC 17025 require on the certificate after an adjustment?
Clause 7.8.4.1 of ISO/IEC 17025:2017 requires that the calibration certificate report the results before and after any adjustment or repair, if available. Those are the as-found and as-left data. Any statement of conformity must follow a decision rule agreed under clause 7.1.3 and reported under clause 7.8.6.
Send us your instrument list and adjustment instructions. Techmaster’s four ISO/IEC 17025 accredited laboratories (ANAB Cert. AC-1736) will quote calibration with as-found and as-left data.
Request a calibration quote

Khanh Nguyen is the Marketing Manager at Techmaster Electronics, a B2B marketing leader covering the test, measurement, and ISO/IEC 17025 accredited calibration industry in the United States.