Quick answer: Measurement traceability is the unbroken chain of comparisons that links a result back to national (NIST) standards, and measurement uncertainty is the quantified doubt, usually reported at about 95% confidence (k=2), around that result. Together they show that a reading is both anchored to a national reference and bounded by how much it can vary. Every Techmaster ISO/IEC 17025 certificate states traceability and a full expanded-uncertainty budget, so your data holds up under audit.
Key points
- Calibration calibration confirms measurements you can defend in an ISO 9001 / 13485 / AS9100 audit.
- Every certificate is NIST-traceable with a full measurement-uncertainty budget (as-found / as-left).
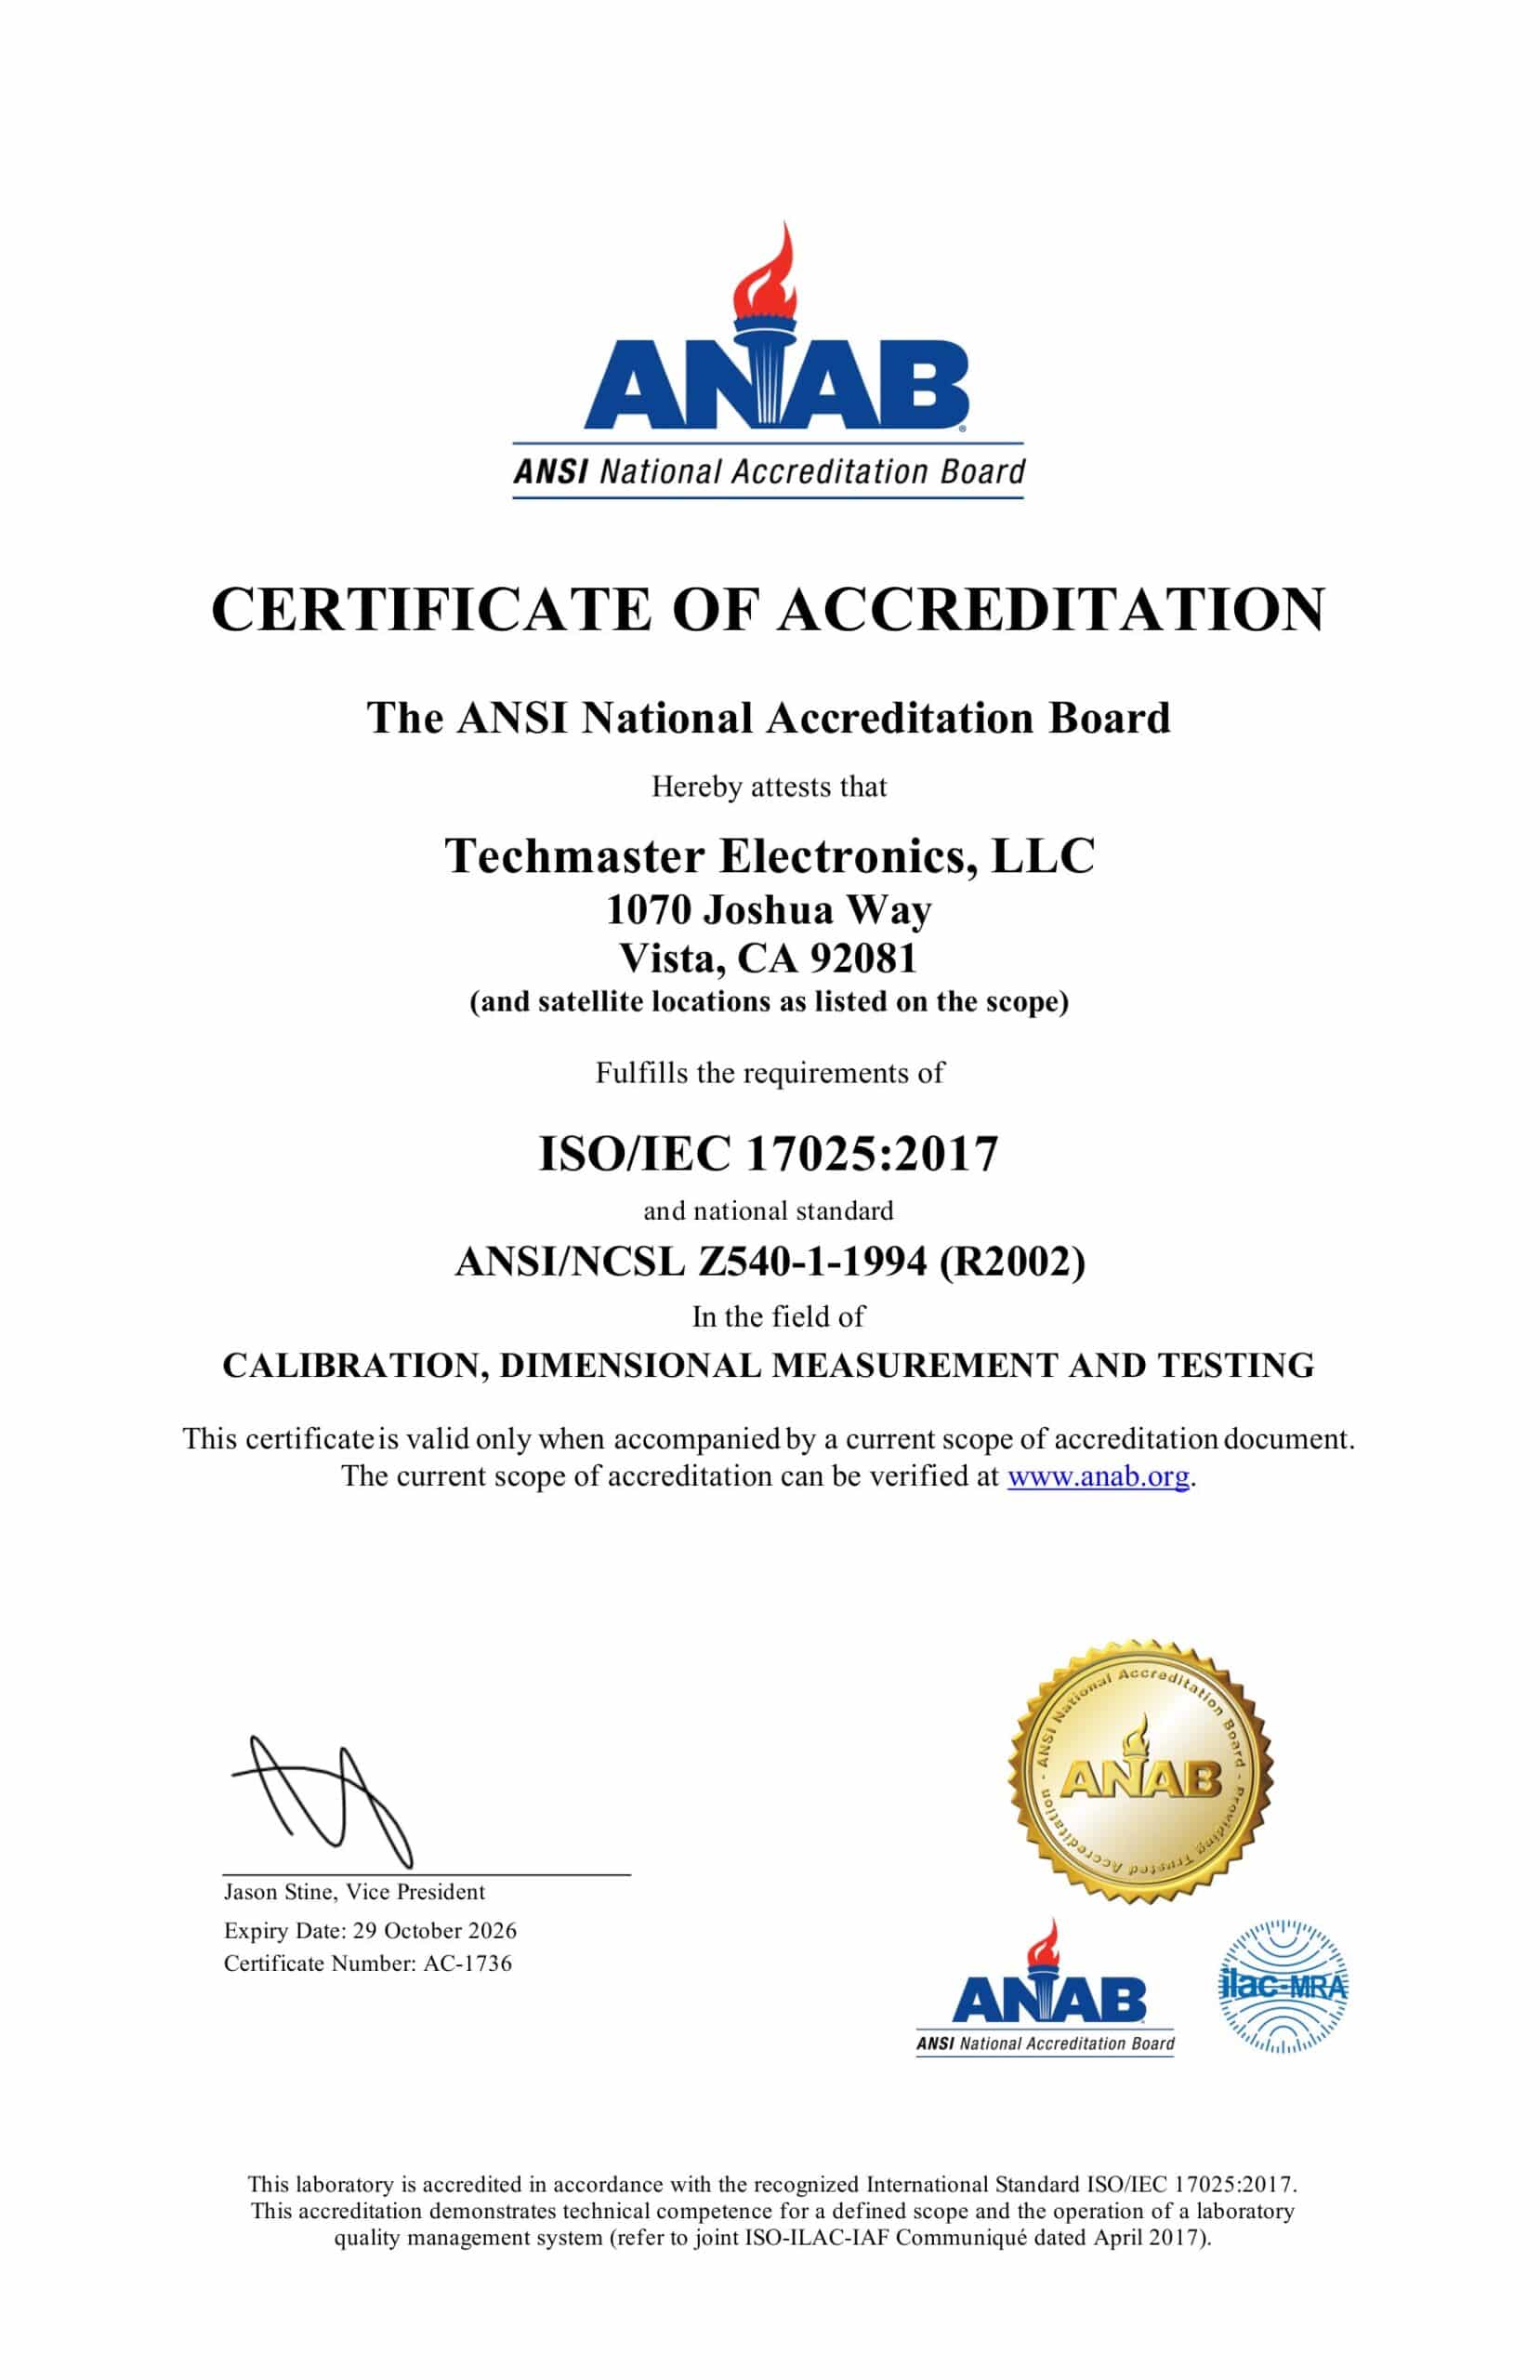
- Techmaster is ANAB-accredited (AC-1736) with five US labs, in-lab or nationwide on-site.
- Standard turnaround is 5 business days, with 1–2 business-day expedite available.
Measurement uncertainty and metrological traceability describe different, connected parts of a result. Uncertainty quantifies the dispersion of values that could reasonably be attributed to the quantity being measured. Traceability connects that result to a stated reference through a documented, unbroken chain of calibrations, with every link contributing uncertainty. Neither term means the instrument is error-free or automatically acceptable for every use.
Uncertainty is not the same as error
Measurement error is the difference between a measured value and a reference quantity value. When a systematic effect is known and significant, a correction may be applied. Uncertainty remains because the reference, method, environment, resolution, repeatability, corrections, and other inputs are not known perfectly.
The International Vocabulary of Metrology defines measurement uncertainty as a non-negative parameter characterizing the dispersion of quantity values attributed to a measurand. It is not a statement that the actual error equals the uncertainty and should not be presented as a guarantee that a true value lies inside every reported interval.

How an uncertainty statement is built
A measurement model identifies the input quantities that affect the result. Their standard uncertainties are evaluated from repeated observations, documented specifications, calibration certificates, resolution, environmental effects, or other defensible information. Sensitivity to each input is considered, correlated terms are handled where relevant, and the components are combined into a combined standard uncertainty.
Expanded uncertainty is commonly reported as U = k × uc, where uc is combined standard uncertainty and k is a coverage factor. NIST Technical Note 1297 explains that, under appropriate assumptions, k = 2 often gives an interval with approximately 95% coverage. The certificate should state the factor and, where applicable, the coverage probability or basis rather than letting the reader infer it.
Worked calibration result
Illustrative example: a digital thermometer indicates 100.18 °C while the assigned reference value under the calibration conditions is 100.05 °C.
| Reported element | Illustrative value | Interpretation |
|---|---|---|
| Indication | 100.18 °C | Value displayed by the item under calibration |
| Reference value | 100.05 °C | Value assigned by the reference system under stated conditions |
| Indication error | +0.13 °C | Indication minus reference value |
| Expanded uncertainty | 0.08 °C | Reported uncertainty associated with the calibration result |
| Coverage factor | k = 2 | Multiplier used to obtain expanded uncertainty from combined standard uncertainty |
A concise result could be written as “indication error +0.13 °C with expanded uncertainty 0.08 °C, k = 2,” together with the method and relevant conditions. The uncertainty qualifies the estimated error; it is not added to the indication as a routine correction. Whether the thermometer conforms depends on the identified specification and decision rule.

The traceability chain behind the result
- The thermometer indication is compared with a reference thermometer or measurement system.
- That reference has its own calibration result and uncertainty linked to a higher-level standard.
- Successive documented calibrations connect the result to an SI realization or another stated reference.
- The uncertainty from each relevant link and from the current measurement process contributes to the final result.
NIST’s traceability policy and FAQ stresses that traceability is a property of the measurement result, not of an instrument, certificate, or laboratory. It also says the result provider must support the claim and the user must judge whether the evidence is adequate.
What to read on a calibration certificate
- Identification: asset, serial number, configuration, sensor, and channel as applicable.
- Measurand and units: the specific quantity and how it was measured.
- Results: reference values, indications, errors or corrections, and whether data are as-found or as-left.
- Uncertainty: value, units, coverage factor, and basis or probability where applicable.
- Method and conditions: enough information to understand the calibration and important influence quantities.
- Traceability support: identified references or an adequate traceability statement and an unbroken documented chain.
- Conformity: only when requested, tied to a stated specification and decision rule.
- Accreditation status: whether the specific result is covered by the laboratory’s scope.

Why traceability does not guarantee conformity
A result can be traceable yet have uncertainty too large for a tight process tolerance. It can also show an error outside the instrument specification. Traceability establishes the documented reference relationship; accreditation evaluates laboratory competence for scoped activities; conformity compares a result with requirements under a decision rule. These are complementary controls.
For decisions near a tolerance boundary, consult the ILAC G8 guidance on decision rules. For a buyer-focused distinction, see accredited versus NIST-traceable calibration.
Why it matters
Measurement confidence
A drifting calibration produces readings that fail under audit scrutiny.
Compliance
ISO 9001, 13485, AS9100 and FDA systems require traceable calibration.
Cost control
Catching drift early prevents scrapped product and failed lots.
Traceability
An unbroken chain to NIST with stated uncertainty makes your data valid.
Accredited calibration at Techmaster
Techmaster Electronics is an ANAB-accredited (Certificate AC-1736) ISO/IEC 17025:2017 calibration laboratory with five US labs, NIST-traceable standards and a full measurement-uncertainty budget on every certificate, in-lab or on-site nationwide. See our calibration services or request a quote.
Frequently asked questions
What is measurement uncertainty and traceability explained?
Measurement Uncertainty And Traceability Explained is the documented comparison of a calibration against NIST-traceable reference standards under ISO/IEC 17025. It quantifies the calibration’s error and measurement uncertainty and confirms it performs within tolerance, with as-found and as-left data on the certificate.
How often should a calibration be calibrated?
Most quality systems calibrate a calibration every 12 months, or sooner after repair, overload, or before critical measurements. Set your interval from the manufacturer spec and your ISO 9001 / 13485 / AS9100 program and drift history.
Is Techmaster’s calibration calibration ISO 17025 accredited?
Yes. Techmaster Electronics is ISO/IEC 17025:2017 accredited by ANAB (Certificate AC-1736). Every calibration calibration is NIST-traceable and issued with a full measurement-uncertainty budget.
What is the turnaround for calibration calibration?
Standard turnaround is 5 business days, with 1–2 business-day expedite available. On-site calibration removes shipping time entirely for calibrations that can’t leave the floor.
Do you calibrate calibrations on-site or in-lab?
Both. Techmaster runs five US labs (Vista CA, Santa Clara CA, Orlando FL, San Antonio TX, Holly Springs NC) and offers nationwide on-site calibration calibration to minimize downtime.
Related calibration guides
Get accredited calibration
ANAB-accredited, NIST-traceable, 5 US labs, in-lab or on-site.
Contact us for a quoteKhanh Nguyen, Marketing Manager, Techmaster Electronics
Writes on ISO/IEC 17025 calibration, metrology and measurement compliance for US labs. Connect on LinkedIn →

Khanh Nguyen is the Marketing Manager at Techmaster Electronics, a B2B marketing leader covering the test, measurement, and ISO/IEC 17025 accredited calibration industry across the US and Vietnam markets.