Surface Plate Calibration
Accuracy across the range
How Surface Plate calibration works
- Intake & visual inspection
- Environmental stabilization
- As-found measurement
- Comparison to NIST-traceable standards
- Adjustment if required
- As-left results & certificate
Your calibration, covered
In-lab vs on-site calibration
In-lab calibration
- Accredited bench with full reference standards
- Best achievable measurement uncertainties
- Pickup & return logistics handled
- Ideal for precision and reference work
On-site calibration
- We calibrate the Surface Plate at your facility
- No shipping risk or transit downtime
- As-found data captured before any move
- Ideal for fixed, large or sensitive assets
In-depth guide
Introduction
In precision manufacturing, accuracy is everything. Even the smallest deviation in measurement can lead to costly rework, product rejection, or compliance issues. At the heart of dimensional measurement lies the surface plate, a seemingly simple granite slab that serves as the foundation for countless quality checks. To maintain reliability, these plates must undergo regular surface plate calibration.
Flatness is one surface property; finish is another, see our guide to surface roughness tester calibration.
This calibration falls under our dimensional calibration service.
This article explains what a surface plate is, why calibration matters, what standards govern the process, and how companies can protect quality by working with accredited calibration service providers.
What is a Surface Plate?
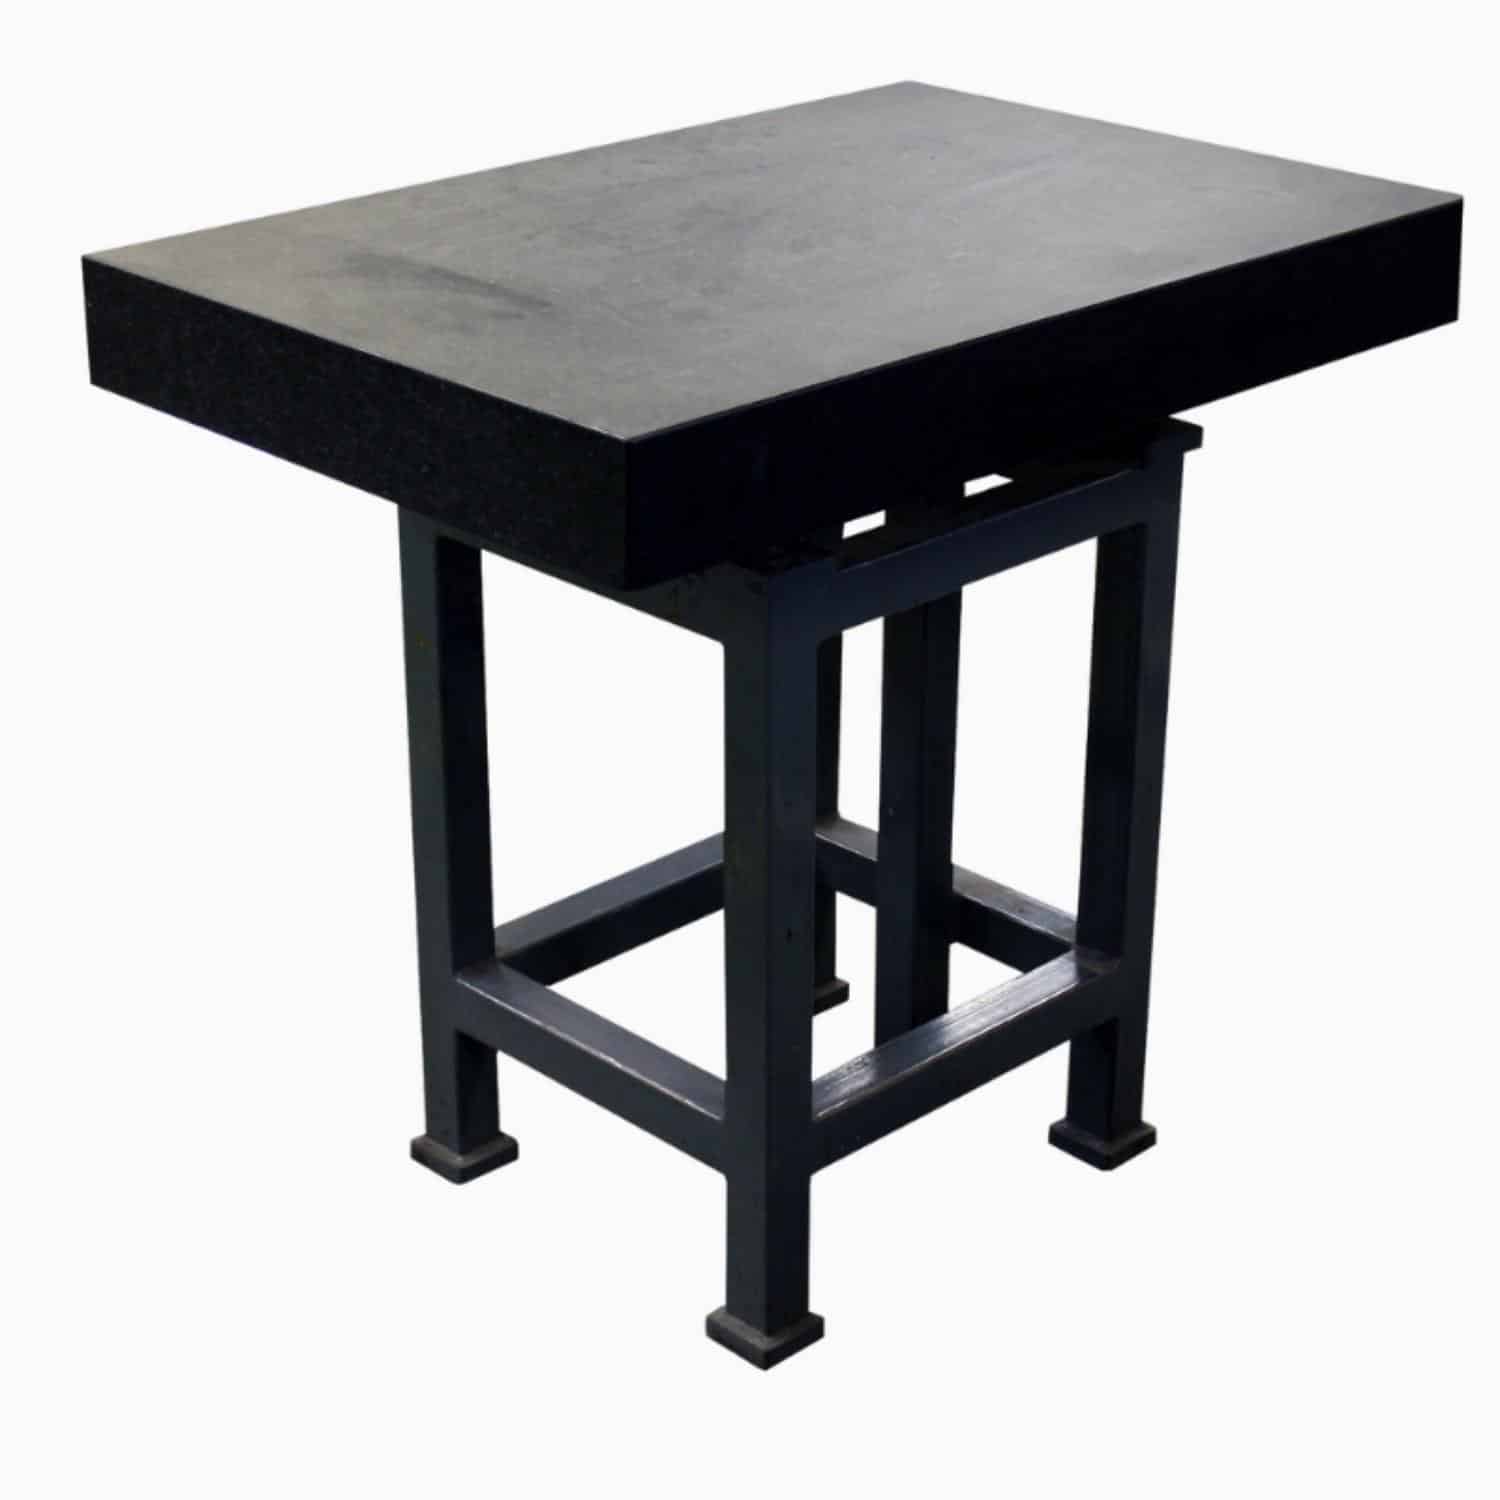
A surface plate is a solid, flat reference plane used in metrology for precise inspection, marking, and layout. Typically made of granite or sometimes cast iron, surface plates provide a stable base against which instruments like micrometers, height gauges, and dial indicators can be checked.
Granite is the preferred material because it resists wear, does not rust, and maintains flatness over time. Surface plates come in various sizes and grades depending on the required accuracy, from small bench-top plates to massive plates installed in inspection labs or workshops.
Applications of Surface Plates
Different audiences rely on surface plates for different reasons:
-
Engineers and Technicians – Use surface plates to calibrate hand tools and ensure day-to-day accuracy of measurements.
-
QA Managers and Procurement Teams – Depend on certified surface plates to prove compliance during audits and maintain customer trust.
-
Beginners or New Engineers – Learn to appreciate the importance of a flat reference plane as the starting point of precision measurement.
Without a properly calibrated surface plate, every measurement taken on it risks being inaccurate, compromising quality at its very foundation.
Why Surface Plate Calibration Matters
Over time, even granite wears down. Dust, chips, accidental impacts, and repeated use can slowly erode flatness. If left unchecked, this leads to:
-
Incorrect measurements – A warped plate gives false readings, causing parts to be incorrectly approved or rejected.
-
Production delays – Faulty measurements cascade into quality issues that halt production lines.
-
Compliance risks – Auditors require proof that reference standards, including surface plates, are calibrated and traceable.
Standards for Surface Plate Calibration (U.S.)
Calibration of surface plates in the United States follows strict industry standards, ensuring results are both consistent and legally defensible. Key standards include:
-
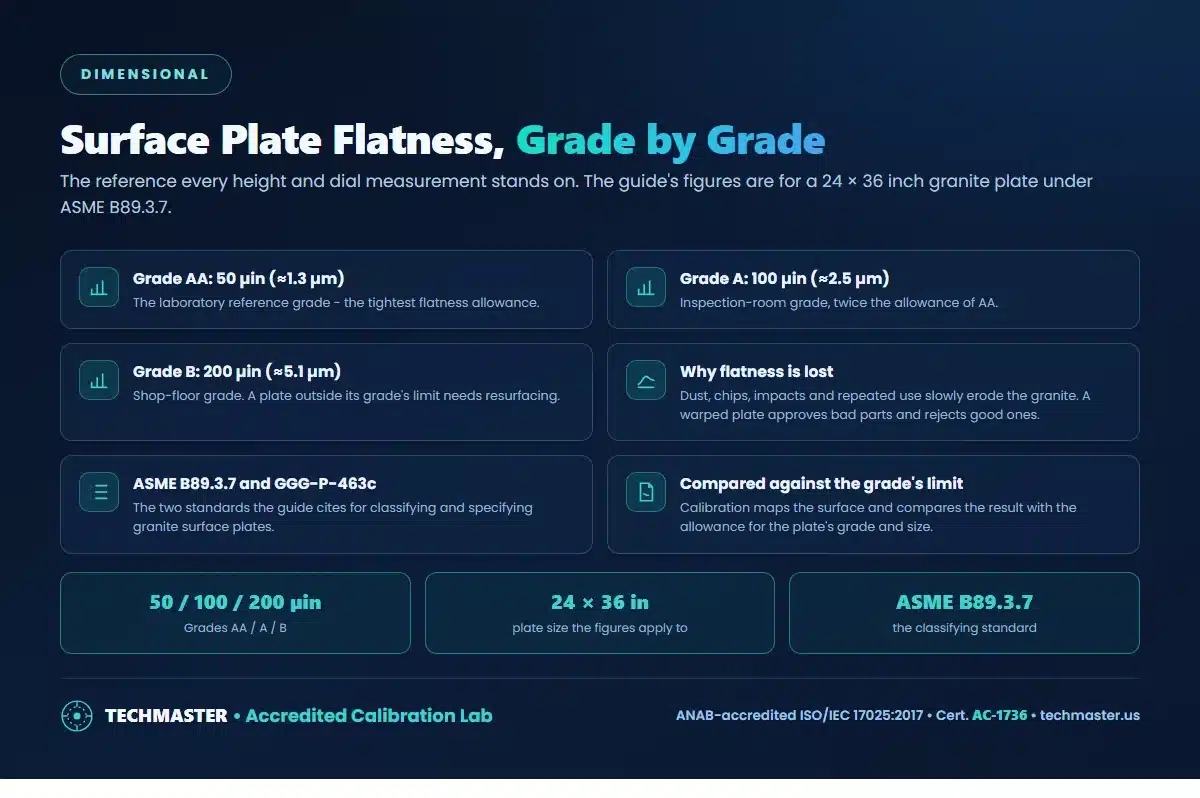
ASME B89.3.7 – Defines accuracy requirements and classification for granite surface plates.
-
Federal Specification GGG-P-463c – Establishes performance standards for granite plates.
-
ISO/IEC 17025 – Accreditation standard for calibration laboratories, ensuring competency and traceability.
-
NIST Traceability – Links measurements back to the U.S. National Institute of Standards and Technology.
Surface plates are classified into Grades:
-
AA (Laboratory Reference) – Highest accuracy, used for calibration labs.
-
A (Inspection Room) – Common in QA environments.
-
B (Workshop) – Suitable for shop-floor use, where tolerances are less strict.
Testing & Calibration Procedures
Surface plate calibration is more than a quick visual check. Accredited labs follow detailed procedures:
-
Visual inspection – Checking for cracks, chips, rust, or damage.
-
Repeat measurement test – Verifying consistency across multiple readings.
-
Autocollimator or electronic level mapping – Measuring flatness across the entire surface using optical or electronic instruments.
-
Flatness evaluation – Comparing results against allowable tolerances for the plate’s grade and size.
-
Certificate issuance – Providing documented proof of compliance with ASME and ISO standards.
Example: A 24×36 inch Grade B surface plate is allowed a maximum deviation of 200 µin (≈ 5.1 µm). If calibration shows deviations beyond this limit, the plate must be re-lapped (precision resurfacing) to restore accuracy.
Surface Plate Flatness Tolerance (24×36 in)
Standard: ASME B89.3.7Comparison of flatness tolerance by grade. Values are typical for a 24×36 inch granite surface plate.
| Grade | Flatness (µin) | Flatness (µm) | Typical Use |
|---|---|---|---|
| AA | 50 µin | ≈ 1.3 µm | Laboratory reference |
| A | 100 µin | ≈ 2.5 µm | Inspection room QA |
| B | 200 µin | ≈ 5.1 µm | Workshop / production |
Measurement Methods & Uncertainty in Calibration
Calibration of surface plates can be performed using different instruments, including:
-
Electronic levels – Detect slope changes across the surface.
-
Autocollimators – Optical devices used for high-precision angular measurement.
-
Laser interferometers – Advanced systems that measure flatness to nanometer resolution.
-
Repeat-o-meter tests – Identify localized wear or “hills and valleys” on the plate surface.
Every calibration has an uncertainty budget, which accounts for factors like instrument accuracy, environmental stability, and operator skill. Understanding this helps QA managers evaluate the reliability of results.
Maintenance & Care for Surface Plates
Even the best-calibrated plate will drift out of tolerance without proper care. Best practices include:
-
Cleaning – Use non-abrasive cleaners and lint-free cloths; never use harsh chemicals.
-
Load management – Avoid concentrated heavy loads; distribute weight evenly.
-
Rotation – Periodically rotate the plate’s working direction to prevent uneven wear.
-
Environmental control – Maintain stable temperature and humidity, avoid direct sunlight or drafts.
-
Daily inspection – Wipe down before and after use to keep dust and oil from affecting measurements.
Common Causes of Flatness Deviation
Several factors accelerate the wear or distortion of surface plates:
-
Improper support – Plates must rest on three-point supports positioned correctly; otherwise, bending or sagging occurs.
-
Thermal gradients – Temperature differences between the top and bottom cause warping.
-
Localized wear – Frequent use in one area leads to uneven flatness.
-
Improper cleaning agents – Chemicals or abrasive pads can damage the surface.
When to Repair or Re-lap a Surface Plate
Calibration not only identifies out-of-tolerance plates but also indicates when resurfacing (re-lapping) is necessary. Indicators include:
-
Measured deviation exceeds the grade tolerance.
-
Visible scratches, chips, or cracks on the working surface.
-
Repeat measurements show inconsistency across zones.
Re-lapping involves grinding the surface with specialized equipment to restore flatness, followed by re-certification.
Case Study: Surface Plate in a QA Lab
A mid-sized metal fabrication company relied on a 24×36 Grade B surface plate in its QA department. Over time, unnoticed wear led to flatness errors beyond specification.
-
Problem: QA inspectors found inconsistent results between tools and rejected parts.
-
Calibration result: Deviation exceeded Grade B tolerance, requiring re-lapping.
-
Outcome: After resurfacing and recalibration, measurement errors dropped, and rejection rates improved by 25%.
Techmaster’s Surface Plate Calibration Services
Techmaster offers professional surface plate calibration services designed to support industries from aerospace to general manufacturing:
-
Onsite service – No need to transport heavy granite plates.
-
ISO/IEC 17025 accredited labs – Traceable to NIST standards.
-
Expert technicians – Skilled in flatness mapping, re-lapping, and certification.
-
Customer portal – Easy access to calibration certificates and schedules.
Whether you manage a workshop with multiple Grade B plates or a laboratory relying on Grade AA standards, Techmaster ensures your equipment meets the highest calibration requirements.
Conclusion & Call to Action
Surface plates may appear simple, but their role in measurement accuracy is foundational. Without regular surface plate calibration, all subsequent inspections and measurements are at risk.
Protect your quality, compliance, and reputation with accredited calibration services you can trust.
Don’t let worn plates compromise your quality, contact Techmaster now for accredited surface plate calibration services you can trust.
Surface Plate Grades, Flatness Methods and Choosing a Calibration Supplier
Most surface plates in US shops are specified to Federal Specification GGG-P-463c or ASME B89.3.7. Both use three grades. The tolerance doubles from one grade to the next, and the allowance grows with the plate’s size:
- Grade AA (laboratory): the tightest flatness tolerance, for gage-block and master-gage work.
- Grade A (inspection): twice the AA tolerance, for inspection rooms and incoming QC.
- Grade B (toolroom): twice the A tolerance, for layout and general shop use.
A certificate should state which grade the plate was checked against, not just print a measured number.
Two measurements, two different questions
Overall flatness asks whether the whole working surface lies between two parallel planes within tolerance. It is mapped with an electronic level, autocollimator or laser system along a grid of lines (often called the Moody or Union Jack pattern), and the data is reduced to a flatness map.
Local-area flatness, or repeat reading, asks whether a gage moved anywhere on the plate reads the same. It is checked with a repeat-reading gage such as a Repeat-O-Meter. A plate can pass overall flatness and still fail repeat reading where it wears in one busy spot, which is exactly where your parts get measured.
On-site, because plates should not travel
Granite plates are heavy, and moving one can change its support and its flatness. They are normally calibrated where they sit, after the plate has had time to settle to room temperature. If a plate fails, the flatness map shows whether the problem is local wear that re-lapping will fix or a plate that should be downgraded or replaced. A plate is also only as useful as what sits on it, so it pays to check the indicators and gage blocks used on it on the same cycle.
What to ask a calibration supplier
- Is surface plate flatness on their ISO/IEC 17025 scope, and for what plate size?
- Do they measure both overall and local-area flatness, and report both against your grade?
- Will you receive the flatness map and the measurement uncertainty, not just pass/fail?
Overall and local-area flatness of surface plates are on Techmaster’s ANAB scope (certificate AC-1736) through our Santa Clara, California dimensional lab.
Frequently asked questions
What is Surface Plate Calibration?
How often should a Surface Plate be calibrated?
What standards apply to Surface Plate Calibration?
What is included on the certificate?
Can you calibrate the Surface Plate on-site?
Need Surface Plate calibration?
ANAB-accredited, NIST-traceable, fast turnaround, in-lab or on-site across the USA.
Contact us for a quoteReferences & industry standards
- ISO/IEC 17025 testing & calibration laboratory requirements
- NIST calibration services and measurement traceability
- NIST RF electromagnetics metrology
- A2LA / ANAB accreditation for calibration laboratories
External standards bodies. Techmaster Electronics is an ISO/IEC 17025-accredited, NIST-traceable calibration laboratory.

Khanh Nguyen is the Marketing Manager at Techmaster Electronics, a B2B marketing leader covering the test, measurement, and ISO/IEC 17025 accredited calibration industry in the United States.